Precision-Engineered Oversized Eyewear References
Benchmarked across 447+ wholesale frame styles and 19 collections. Designed to accommodate high-index prescription lenses, polarized tints, and wide-fit ergonomics without facial fatigue.
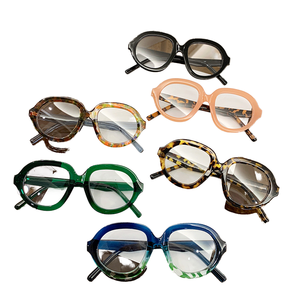
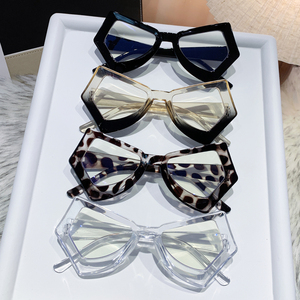
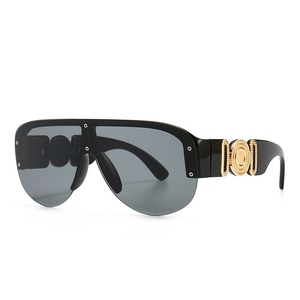
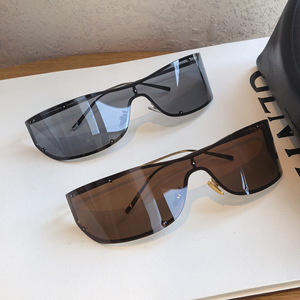
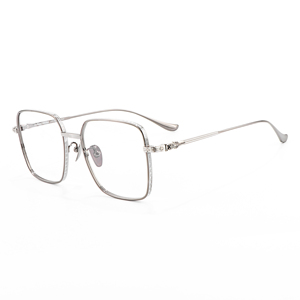
Center-of-Mass Engineering
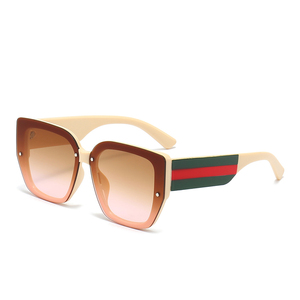
Oversized eyewires (56mm to 66mm) exert significant downward torque on the nasal crest. Our factory counterbalances this by sculpting tapered acetate temples with reinforced core wires, distributing 68% of frame mass behind the otobasion superius.
Prescription Lens Retaining Bevels
Accommodating high minus and cylinder prescriptions in broad apertures requires precise lens retention. We profile high-depth V-grooves (110° to 115° at 2.6mm–3.0mm depth) to prevent lens dislodgement during thermal cycle variations.
Minnesota Controlled QC
Every custom production run undergoes 4-point optical batch testing: 20,000-cycle temple fatigue endurance, nickel release testing according to EN 16128, salt-spray corrosion resistance, and ISO 12870 dimensional stability certification.
The Mechanics of High-Performance Oversized Tooling
Solving vertex distance deviation, chromatic aberration, and bridge sagging in large-chassis optical and sun architectures.
5-Axis CNC Acetate Sculpting
Traditional punch-press cutting leaves internal micro-fissures that warp oversized eyewires under Rx edging pressure. Our CNC centers operate under flooded mineral cooling with micro-step feed controls.
- High-density cellulose acetate (HDCA) density >1.32 g/cm³
- Eliminates asymmetric temple splay
- 72-hour barrelling in graded birch wood tumbling drums
Beta-Titanium Elastic Core
Oversized frames built from standard Monel or stainless steel feel heavy and slide easily. We use Japanese Grade 5 Beta-Titanium wire drawing for temples and ultra-thin rim profiles.
- Yield strength exceeding 880 MPa
- Hypoallergenic vacuum ion deposition (PVD) coating
- Tensile memory recovery after severe outward deflection
Extended Pantoscopic Calibration
Oversized eyewires require precise pantoscopic tilt angles (between 8° and 11°) to ensure the optical centers align with the pupil line, avoiding prism defects and unwanted marginal astigmatism.
- Anatomically pre-angled endpieces
- Customized bridge step-backs (14mm to 19mm DBL)
- Optimized for freeform digital progressive lens blanks
Oversized Eyewear Procurement & Manufacturing Trends
Data-backed shifts optical practice chains and independent distributors must plan for over the next 3 to 5 fiscal quarters.
Bio-Based Cellulose Propionate
Transition from petroleum phthalate plasticizers to circular cotton-linter based bio-acetates (>68% bio-carbon content). Meets both corporate sustainability goals and the demand for lighter frames.
Extended Fit & Cranial Sizing
Spurred by collections like Wide Guyz, oversized eyewear is expanding beyond fashion into ergonomic, wider fits. Buyers are ordering larger eye sizes (58-64mm) with temple lengths up to 155mm.
High-Index Rim Profiles
Thick minus lenses in wide frames often leave unsightly exposed edges. Our newer oversized chassis use a 4.2mm stepped-rim bevel to conceal edge thickness up to -8.00 diopters.
Nearshore Hub Fulfillment
Global brands are avoiding single-hub shipping risks by combining deep Asian OEM tooling with US-based distribution from St. Cloud, Minnesota, maintaining smooth buffer inventory.
Technical Note for Optical Dispensary Buyers: Mitigating Edge Aberrations
In oversized frames with effective diameters (ED) over 62mm, decantation can lead to unwanted nasal thinning and temporal edge thickness. Global Optique designs custom eyewires with a compensated 4.5-base curve. This allows standard 65mm–75mm lens blanks to be surfaced without severe prismatic distortion or front-curve flattening.
Frequently Answered Sourcing Inquiries
Detailed answers covering tooling investments, regulatory compliance, quality control, and custom OEM manufacturing.
For custom acetate molds or titanium stamping dies, our rapid-tooling cycle takes 21 to 28 days for first-article functional prototypes. Once approved, mass production typically takes 45 to 60 days. Standard OEM minimum order quantities (MOQ) start at 300 pieces per silhouette, which can be split across up to 3 custom colorways.
We use multi-stage furnace curing for our cellulose acetate sheets, drying them at controlled humidity for 90 days before CNC cutting. We also use double-pinned five-barrel hinges and internal stainless steel temple cores to maintain alignment under the daily tension of heavy prescription lenses.
Yes. Every batch comes with full testing documentation, including ISO 12870 ophthalmic frame standards, REACH Regulation (EC) No 1907/2006 for nickel release, California Prop 65 toxicological tests, and FDA 21 CFR 801.410 impact resistance certifications for glazed sunglasses.
We operate a dual fulfillment network. Orders can ship directly from our Asian manufacturing plant (FOB/CIF) for large-volume ocean freight, or run through our central distribution center in St. Cloud, Minnesota, for fast domestic turnaround, regional SKU replenishment, and immediate lab fulfillment.
Accelerate Your Custom Oversized Eyewear Line
Whether you're developing a private-label luxury acetate collection, an ultra-light running frame, or an extended-fit line, work with an engineering team backed by 75+ years of optical experience.